Switchgear Tulip Contact ODM: Precision Manufacturing for Reliable Electrical Performance
2026-09-15
In the demanding world of switchgear, the tulip contact is more than a component—it's a linchpin for reliable electrical performance. Yet, achieving the precision required for flawless operation is no small feat. That's where MOLDVOLT steps in, bringing ODM expertise that transforms complex design challenges into reliable, high-precision solutions. From material selection to final tolerance control, every step is engineered to keep your switchgear running at its best. Curious how precision manufacturing elevates electrical reliability? Read on.
Why Tulip Contact Slots Demand Tight Tolerances
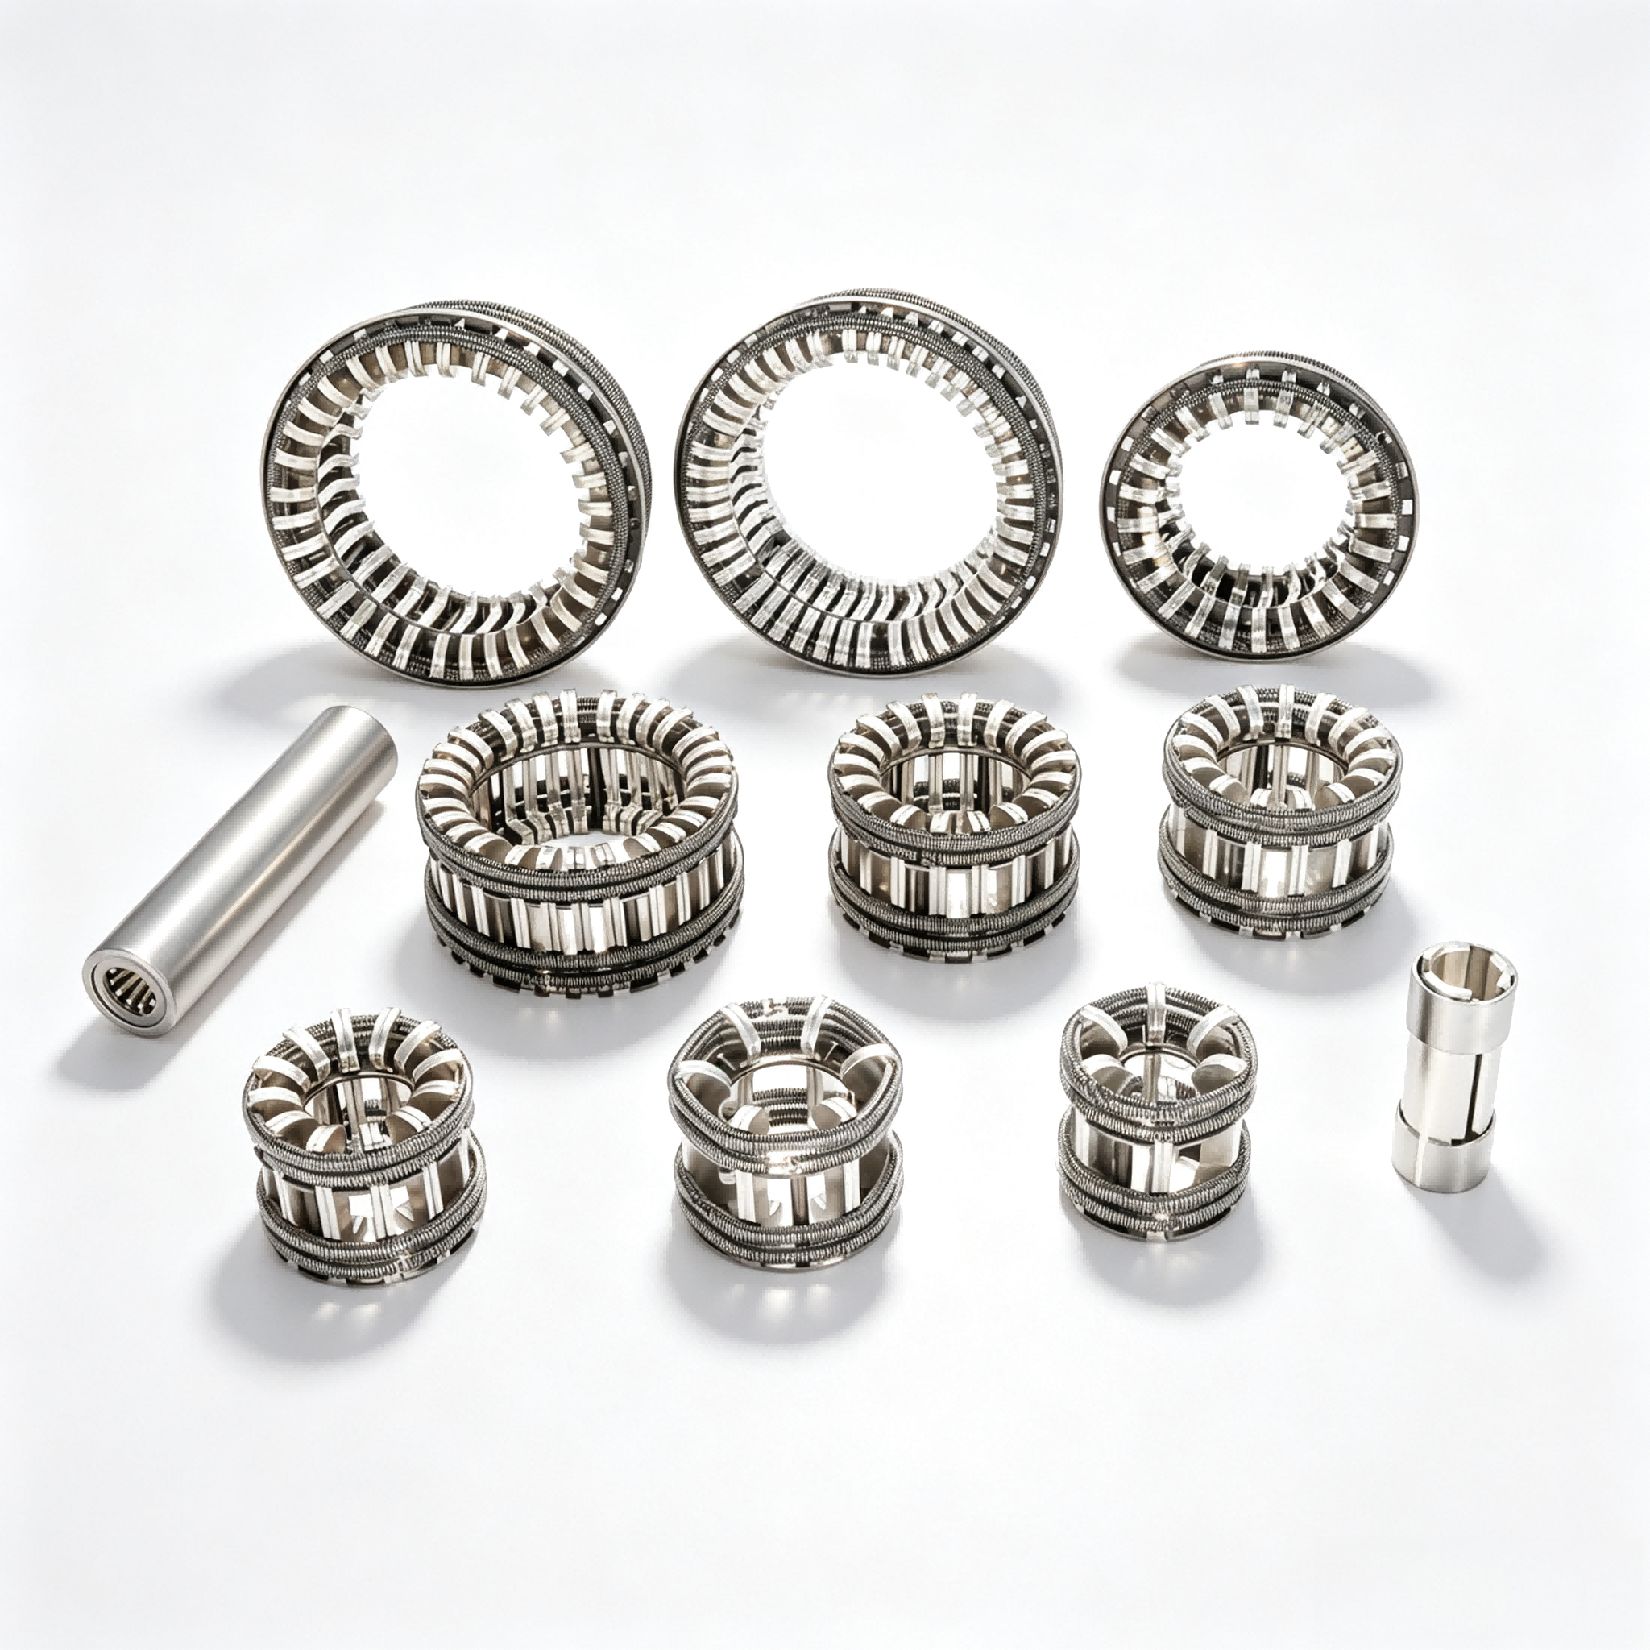
A tulip contact slot relies on several spring fingers arranged radially to grip a mating pin. Each finger must deflect by nearly the same amount; if one finger is slightly longer or the slot slightly wider on one side, that finger may carry most of the normal force while its neighbours barely touch. Tight tolerances keep the finger geometry and slot diameter within a narrow band so the contact force distributes evenly, which directly limits hot spots and localised wear.
The forming process for these slots involves stamping and rolling thin copper alloy strip into a barrel shape. Springback after forming is never perfectly repeatable, so small variations in the tooling or material temper can shift the slot opening by more than the intended clearance. A slot that opens too wide lowers insertion force but sacrifices contact pressure; one that closes too much scrapes or jams the pin. Specifying tight dimensional limits forces manufacturers to control the forming variables that matter most.
Over repeated mating cycles and temperature swings, minor geometric errors accumulate. A slot that begins life at the edge of a loose tolerance may still pass initial testing but develop intermittent contact after thermal expansion relaxes the spring fingers. Tight tolerances reduce this margin for early degradation, preserving stable contact resistance and preventing fretting corrosion when vibration or thermal cycling is present.
Matching Base Materials to Electrical and Thermal Stress
A laminate that handles electrical stress well may still crack under thermal cycling, so the selection process has to weigh both sides simultaneously. For high-voltage boards, the material's dielectric breakdown strength and comparative tracking index (CTI) are the first gatekeepers. Thin, resin-rich cores often rate lower on CTI than glass-heavy alternatives, and surface contamination can push a marginal material into arc tracking territory. Designers frequently overlook that AC stress at elevated temperatures accelerates insulation aging far more than either factor alone.
On the thermal side, a substrate's glass transition temperature (Tg) and decomposition temperature (Td) only tell part of the story. Through-hole assemblies and heavy copper pours generate localized hotspots that demand better thermal conductivity than standard FR-4 provides. Mismatched coefficients of thermal expansion between the copper, laminate, and solder mask create shear strain on plated vias, which is a leading cause of field failures in power electronics. Ceramic-filled hydrocarbon and polyimide-based materials earn their cost premium by keeping that strain within acceptable limits across thousands of cycles.
Sometimes the right choice isn't the highest-spec sheet number. A material with excellent thermal endurance but poor adhesion to heavy copper or a low-Tg option that still passes vibration testing may fit better once assembly processes and operating environment are factored in. The key is matching the failure modes you're actually designed against—not just chasing a higher Tg on paper.
How Multi-Axis Machining Improves Contact Uniformity
Multi-axis machining inherently reduces the number of setups required to produce a component, which directly affects how evenly mating surfaces meet. Every time a part is repositioned, tiny registration errors can creep in, leaving behind subtle steps or misalignments. By keeping the workpiece fixed and rotating the cutting tool around it, a five-axis machine can machine all critical contact faces in a single continuous operation. This approach preserves dimensional continuity and keeps surface profiles consistent, so that when two components come together, pressure distributes evenly rather than concentrating on a few high spots.
The ability to tilt the tool also lets manufacturers reach complex geometries without resorting to longer, thinner cutters that deflect under load. A shorter tool can maintain a constant engagement angle across curved or angled surfaces, producing a finish with less variation in peak-to-valley height. For sealing faces, valve seats, or bearing journals, this translates into fewer microscopic gaps and a larger actual contact area. The result is not just a smoother texture but a more predictable one, where the surface interacts with its counterpart in the same way across its entire footprint.
Beyond geometry, multi-axis paths can be programmed to follow the natural contours of a part rather than stepping over them in a flat raster pattern. This contour-parallel strategy keeps cutting forces stable and reduces the risk of localized chatter or tool dwell marks that might otherwise create hard spots or uneven material removal. Combined with the reduced handling errors from fewer setups, the improvement in contact uniformity comes from a chain of small advantages: better alignment, tighter form tolerances, and a consistent surface texture that holds up under real load conditions.
Prototyping Tulip Contacts Without Overcommitting Inventory
Early-stage tulip contact designs rarely survive first contact with real manufacturing constraints. Rather than locking in large material buys, lean on small-batch metal stamping and 3D-printed forming tools. These let you iterate on spring force, plating thickness, and insertion feel without carrying thousands of units that might end up as scrap.
A practical trick is to split the prototype into two parts: the contact body and the tulip cage. Machine or print the cage in a few variants, then test with off-the-shelf pins or simple turned contacts. This keeps your custom inventory nearly zero while still giving honest feedback on retention and mating cycles.
Only after a design passes repeated insertion and extraction tests should you move to a pilot run. Even then, consider shared tooling or modular dies that can be tweaked later. Overcommitting inventory early almost always means paying twice: once for the parts you didn't need, and again for the redesign you couldn't avoid.
What In-House Testing Reveals Before Customer Sign-Off
Internal test cycles tend to surface the issues that matter most once real users get involved. A feature that looks complete on the requirement sheet often falls apart when two modules interact under load, or when someone follows an unexpected click path. In-house testing brings these failure modes into the open early—before they become expensive fixes or awkward conversations during customer acceptance.
Beyond functional bugs, in-house runs expose gaps in documentation, unclear error messages, and setup steps that only work on a developer's machine. These are rarely captured in formal specs but frequently shape the first impression a customer forms. By documenting what actually breaks and what was assumed, the team enters sign-off with a clearer picture of residual risk and a shorter list of surprises.
Adapting ODM Designs for Retrofit and New Switchgear
Retrofitting existing switchgear with ODM components rarely follows a straight path. Older panels often carry legacy busbar layouts, outdated protection relays, and dimensional quirks that standard catalog parts simply ignore. A practical approach starts with a detailed dimensional and electrical audit of the installed base, then translates those findings into ODM design adjustments—custom busbar offsets, revised mounting frames, or reconfigured cable compartments—so the new modules slide in without forcing a complete shutdown or costly civil work.
For new switchgear, ODM adaptation focuses less on fitting into tight corners and more on building in flexibility from day one. That means specifying modular breaker trucks, plug-in control wiring, and scalable busbar ratings that let the same core design cover multiple project voltages and fault levels. It also involves close collaboration with the ODM partner on thermal performance and type-test documentation, ensuring that changes made for one client do not silently erode the design margins another site depends on.
FAQ
They provide a large number of independent contact points in a compact cylindrical form, which keeps current density low and helps the joint survive short-circuit forces without welding or excessive heating. The segmented fingers also adapt to slight misalignment during breaker racking.
Our involvement starts at the design review stage, checking finger geometry, spring force, and housing tolerances against your rated current and fault level. Then we handle material selection, prototyping, type-test support, and finally volume production with full dimensional and electrical inspection reports.
We typically use high-conductivity copper alloys like CuCrZr or CuNiSi, depending on the mechanical load and operating temperature. For high-fault-duty designs, the fingers are often silver-plated to 8-12 microns to reduce oxidation and keep insertion force stable over thousands of operations.
Contact force from each finger spring is verified on every batch, not just sampled. We also check surface finish and plating thickness on the contact areas, and in-process tests measure voltage drop at rated current to catch any abnormal heating before the parts leave the line.
Yes. The finger count, cross-section, spring arrangement, and terminal geometry can all be adjusted. We frequently supply variants from a few hundred amps up to several thousand amps, including designs with flat pad, threaded stud, or bolted blade terminations.
We run mechanical endurance and temperature-rise tests according to the relevant IEC or ANSI standards. That includes repeating insertion and withdrawal cycles while monitoring contact resistance, then performing short-time current tests on representative samples to confirm no welding or structural deformation occurs.
We freeze a detailed technical datasheet after the first design review, including material grades, plating thickness, spring characteristics, and critical dimensions. Any changes after that require a formal deviation note, so the timeline stays predictable and the final parts match the approved samples.
Check the consistency of finger spacing, the quality of the plating on the inner contact surface, and whether the supplier provides measured spring force and voltage drop data for each lot. A well-made tulip contact will have uniform insertion force and no visible tool marks on the current-carrying faces.
Conclusion
Tulip contacts in switchgear cannot afford loose tolerances. The slots must grip mating components with consistent contact pressure, or localized heating and premature wear become inevitable. Our ODM process treats every slot dimension as a functional parameter, not just a drawing number. By combining tight machining allowances with material grades selected for thermal and electrical duty, we keep resistance low and heat dissipation predictable. Multi-axis machining then removes variation across the contact fingers, so each tulip behaves like its neighbor under fault-level current.
Prototyping doesn't have to mean stocking large batches of uncertain designs. We build functional samples from production-grade alloys and run in-house cyclic, temperature-rise, and insertion-force tests before any customer sign-off. This reveals how a contact will perform in real switchgear, not just how it looks on a CMM report. When an existing installation needs new tulips or a new panel needs a custom interface, the same process adapts without re-engineering the surrounding assembly. The result is a contact set that fits first time and keeps performing through years of switching operations.
Contact Us
Contact Person: Hellen
Email: [email protected]
Tel/WhatsApp: 86-13634205622
Website: https://www.voltcabinet.com